Make OEE the starting point for production improvement.
Bring machine data and operator context into one reliable view. See what is limiting availability, performance and quality, and decide where improvement should start.
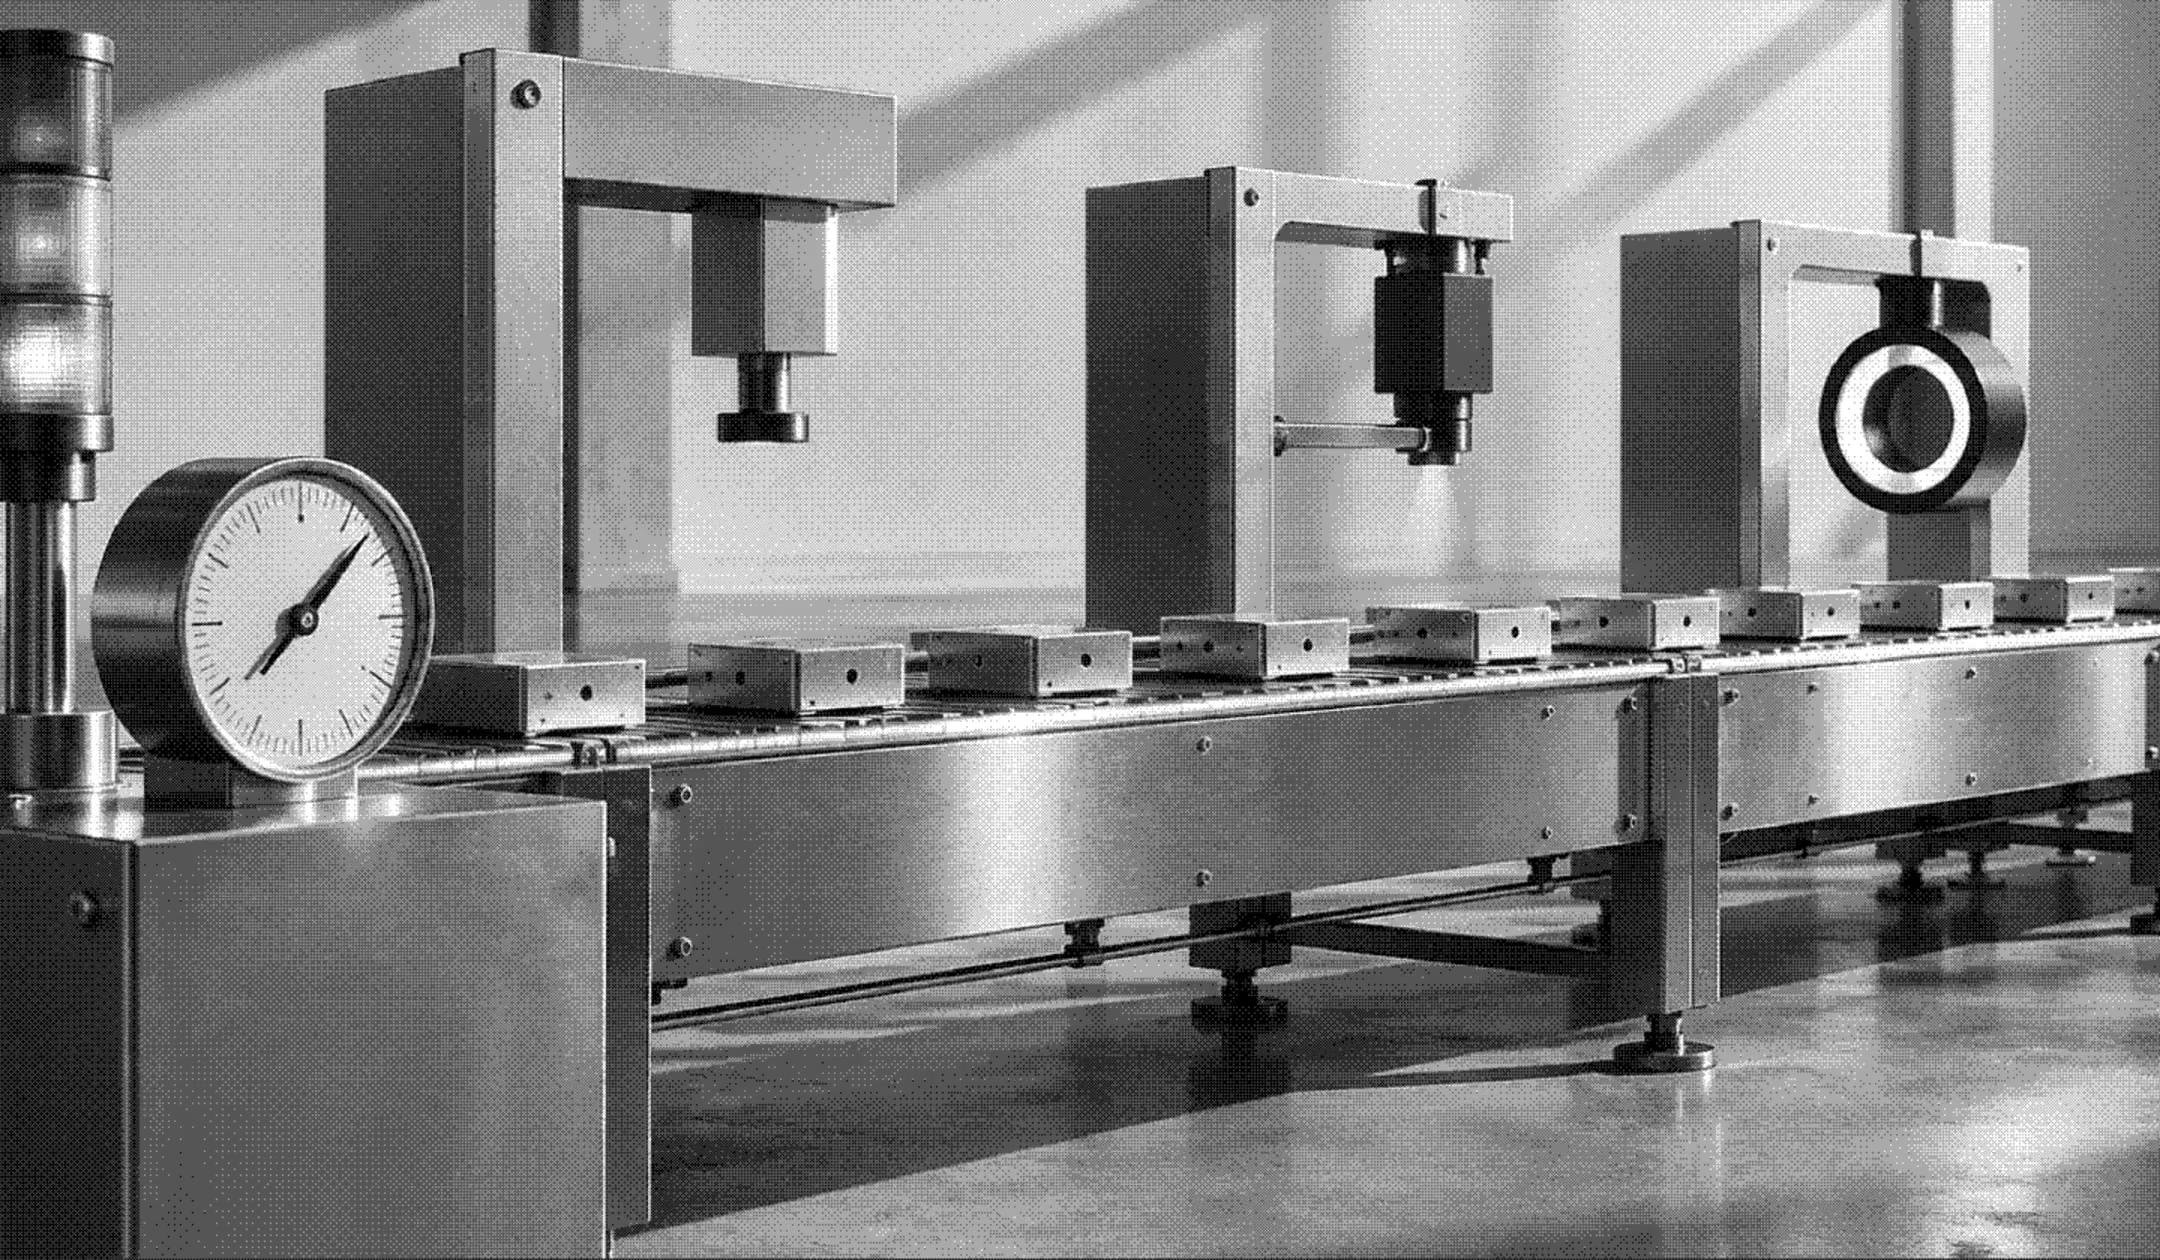
Knowing your OEE is not the same as knowing what to improve.
When a line delivers less than planned, the impact reaches far beyond the OEE score. Production costs rise, schedules become harder to meet and operators are held back by constraints they cannot resolve alone.
OEE should help explain that gap and show where improvement can create the most value. Too often, the way it is measured and understood gets in the way.
Where OEE often falls short
- OEE is calculated differently across teams and sites, making the number difficult to trust.
- Machine data shows when output was lost, but often not why.
- Losses are reported, but not translated into clear priorities and follow-up actions.
Define good production before you calculate OEE.
We do not start from a standard percentage or industry benchmark. OEE only becomes meaningful when planned time, expected speed and good output reflect how your production is intended to run.
From there, machine signals and knowledge from the floor can show which losses matter and where improvement should begin.
Agree on the OEE definition
Establish how availability, performance and quality are calculated for your production.
--
Calculate OEE in production context
Compare products, recipes, lines and shifts at a meaningful level instead of relying on one overall average.
--
Capture the reason, not just the event
Detect stops and slowdowns automatically and add the operational context machines cannot provide.
--
Close the loop on improvement
Turn recurring losses into actions and follow up on whether those actions improved production.
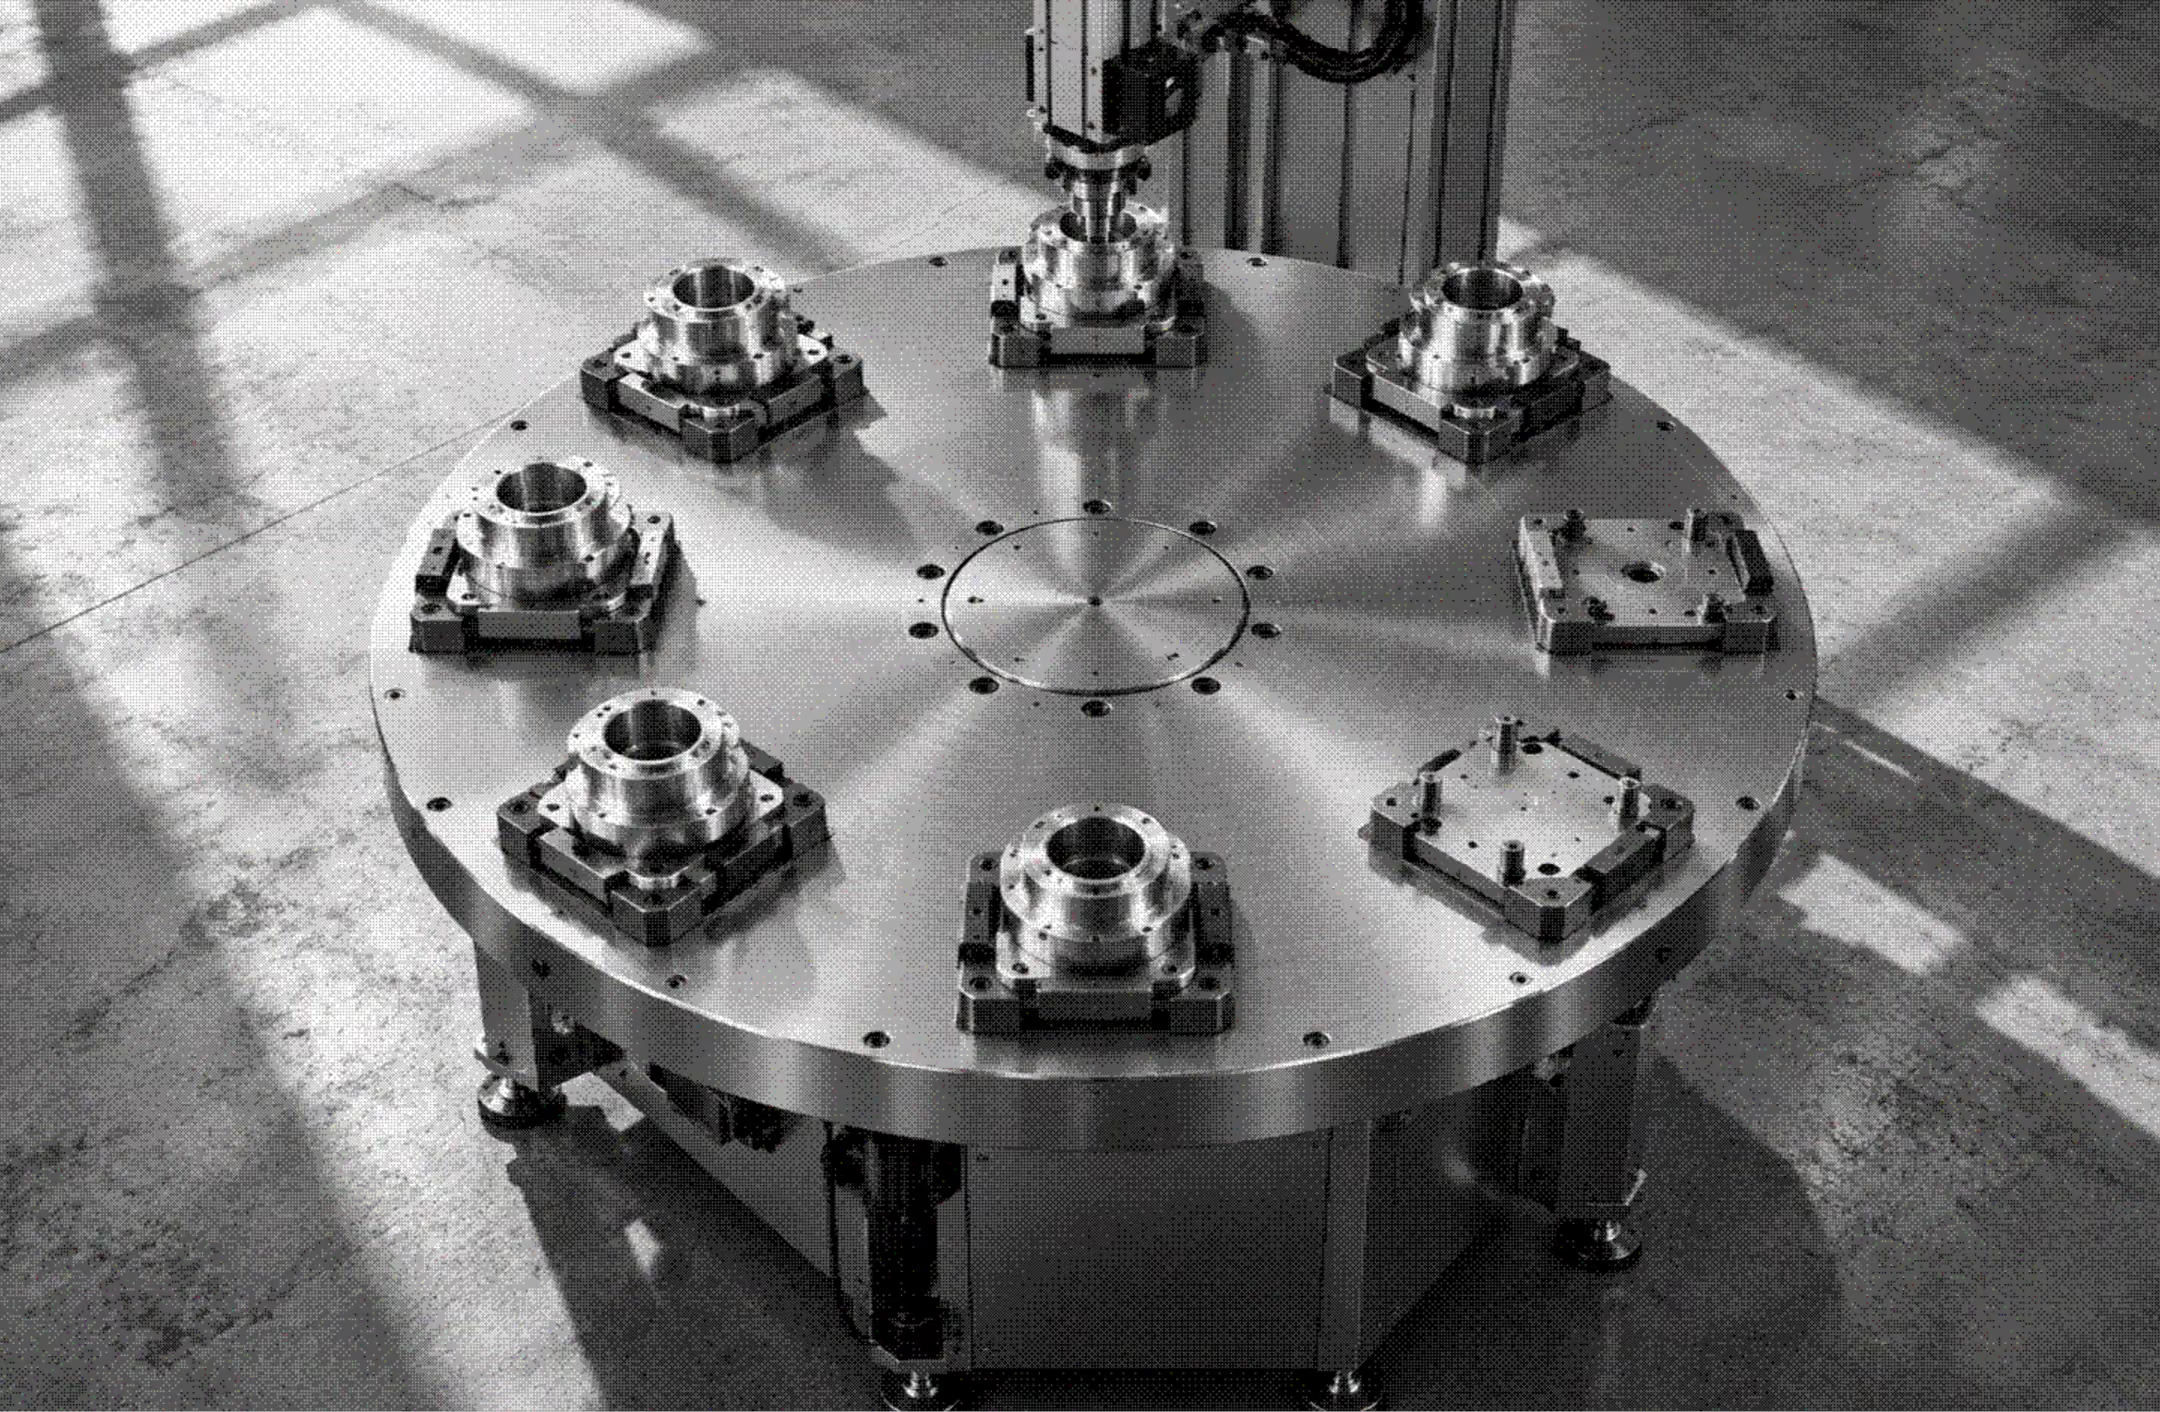

Capture the context machines cannot provide.
Machine signals can detect stops, slowdowns and output, but they do not always explain their cause. We create simple operator workflows that add reason codes and production context without turning registration into extra administrative work.

Show where production is losing performance.
Calculate OEE from the agreed availability, performance and quality definitions. Analyse the result by line, product or shift so teams can see which loss is driving the overall score.

Bring the production signals together.
Connect machines and production systems to capture runtime, stops, output and quality data. Structure those signals consistently, making the inputs for OEE easier to interpret and compare.
Turn OEE into a shared improvement agenda.
Reliable OEE gives teams a shared basis for improvement. The conversation moves beyond the score to which production loss deserves attention first.
Lower the cost of lost output.
See whether availability, performance or quality is limiting output, and focus improvement on the losses with the greatest cost impact.
--
Make batch output more predictable.
Reliable OEE shows what a line typically delivers, helping teams forecast batch output, plan more realistically and reduce the extra stock needed to absorb production fluctuations.
--
Show operators the impact of their work.
When operators can see what held the line back and whether improvements worked, OEE becomes useful feedback that keeps them involved in improvement.
From the shop floor, into practice.
Energy management with Etex
Etex used data analysis to cut energy waste at its plasterboard plants, uncovering excess consumption after every production downtime.
How PSS built a digital manufacturing culture with a custom Mendix MES
How do you build a digital culture that operators actually embrace and keep using? Premium Sound Solutions produces 120 million speakers a year across six global plants for automotive and consumer goods where traceability and quality are non-negotiable.
Sibelco - Workorder Execution App
As Sibelco’s Mendix partner, we co-created their first native low-code app to streamline their maintenance management and integrate it with SAP S/4HANA. The resulting app has improved operating efficiency for technicians, planners and supervisors throughout the organisation.
Terumo's traditional Japanese decision-making process (Ringi) kick-started their low-code journey
Terumo, a global leader in medical technology and innovation, began their low-code adventure by reimagining the Japanese business practice of ringi in the digital era. From there we moved to manufacturing, using Mendix to stream-line their shop floor in Leuven and beyond.
A few things you may want to know.
Learn more about how Mayker scopes, builds and supports applications for production environments.
OEE stands for Overall Equipment Effectiveness and is calculated by multiplying availability, performance and quality. Together, these show how much of the planned production time resulted in good output at the expected speed.
The OEE formula stays the same, but teams may use different assumptions for planned production time, target speed and good output. Agreeing on those inputs first makes OEE easier to trust, compare and use as a basis for improvement.
A line may produce different products, recipes and batch sizes, each with its own expected speed, quality profile and changeover pattern. Analysing OEE by product, order or batch helps teams compare similar production runs and see what is really driving the difference.
Machine data can show runtime, stops, speed and output, but it rarely provides the complete explanation. Connecting those signals with the production order, product or recipe, batch and operator input reveals what happened and why.
OEE is most useful when machines or automated processes have a meaningful impact on production cost, capacity or delivery performance. Start where lost output has the greatest financial or operational impact, rather than measuring every asset simply because you can.